Advanced Chemical Materials at Scale
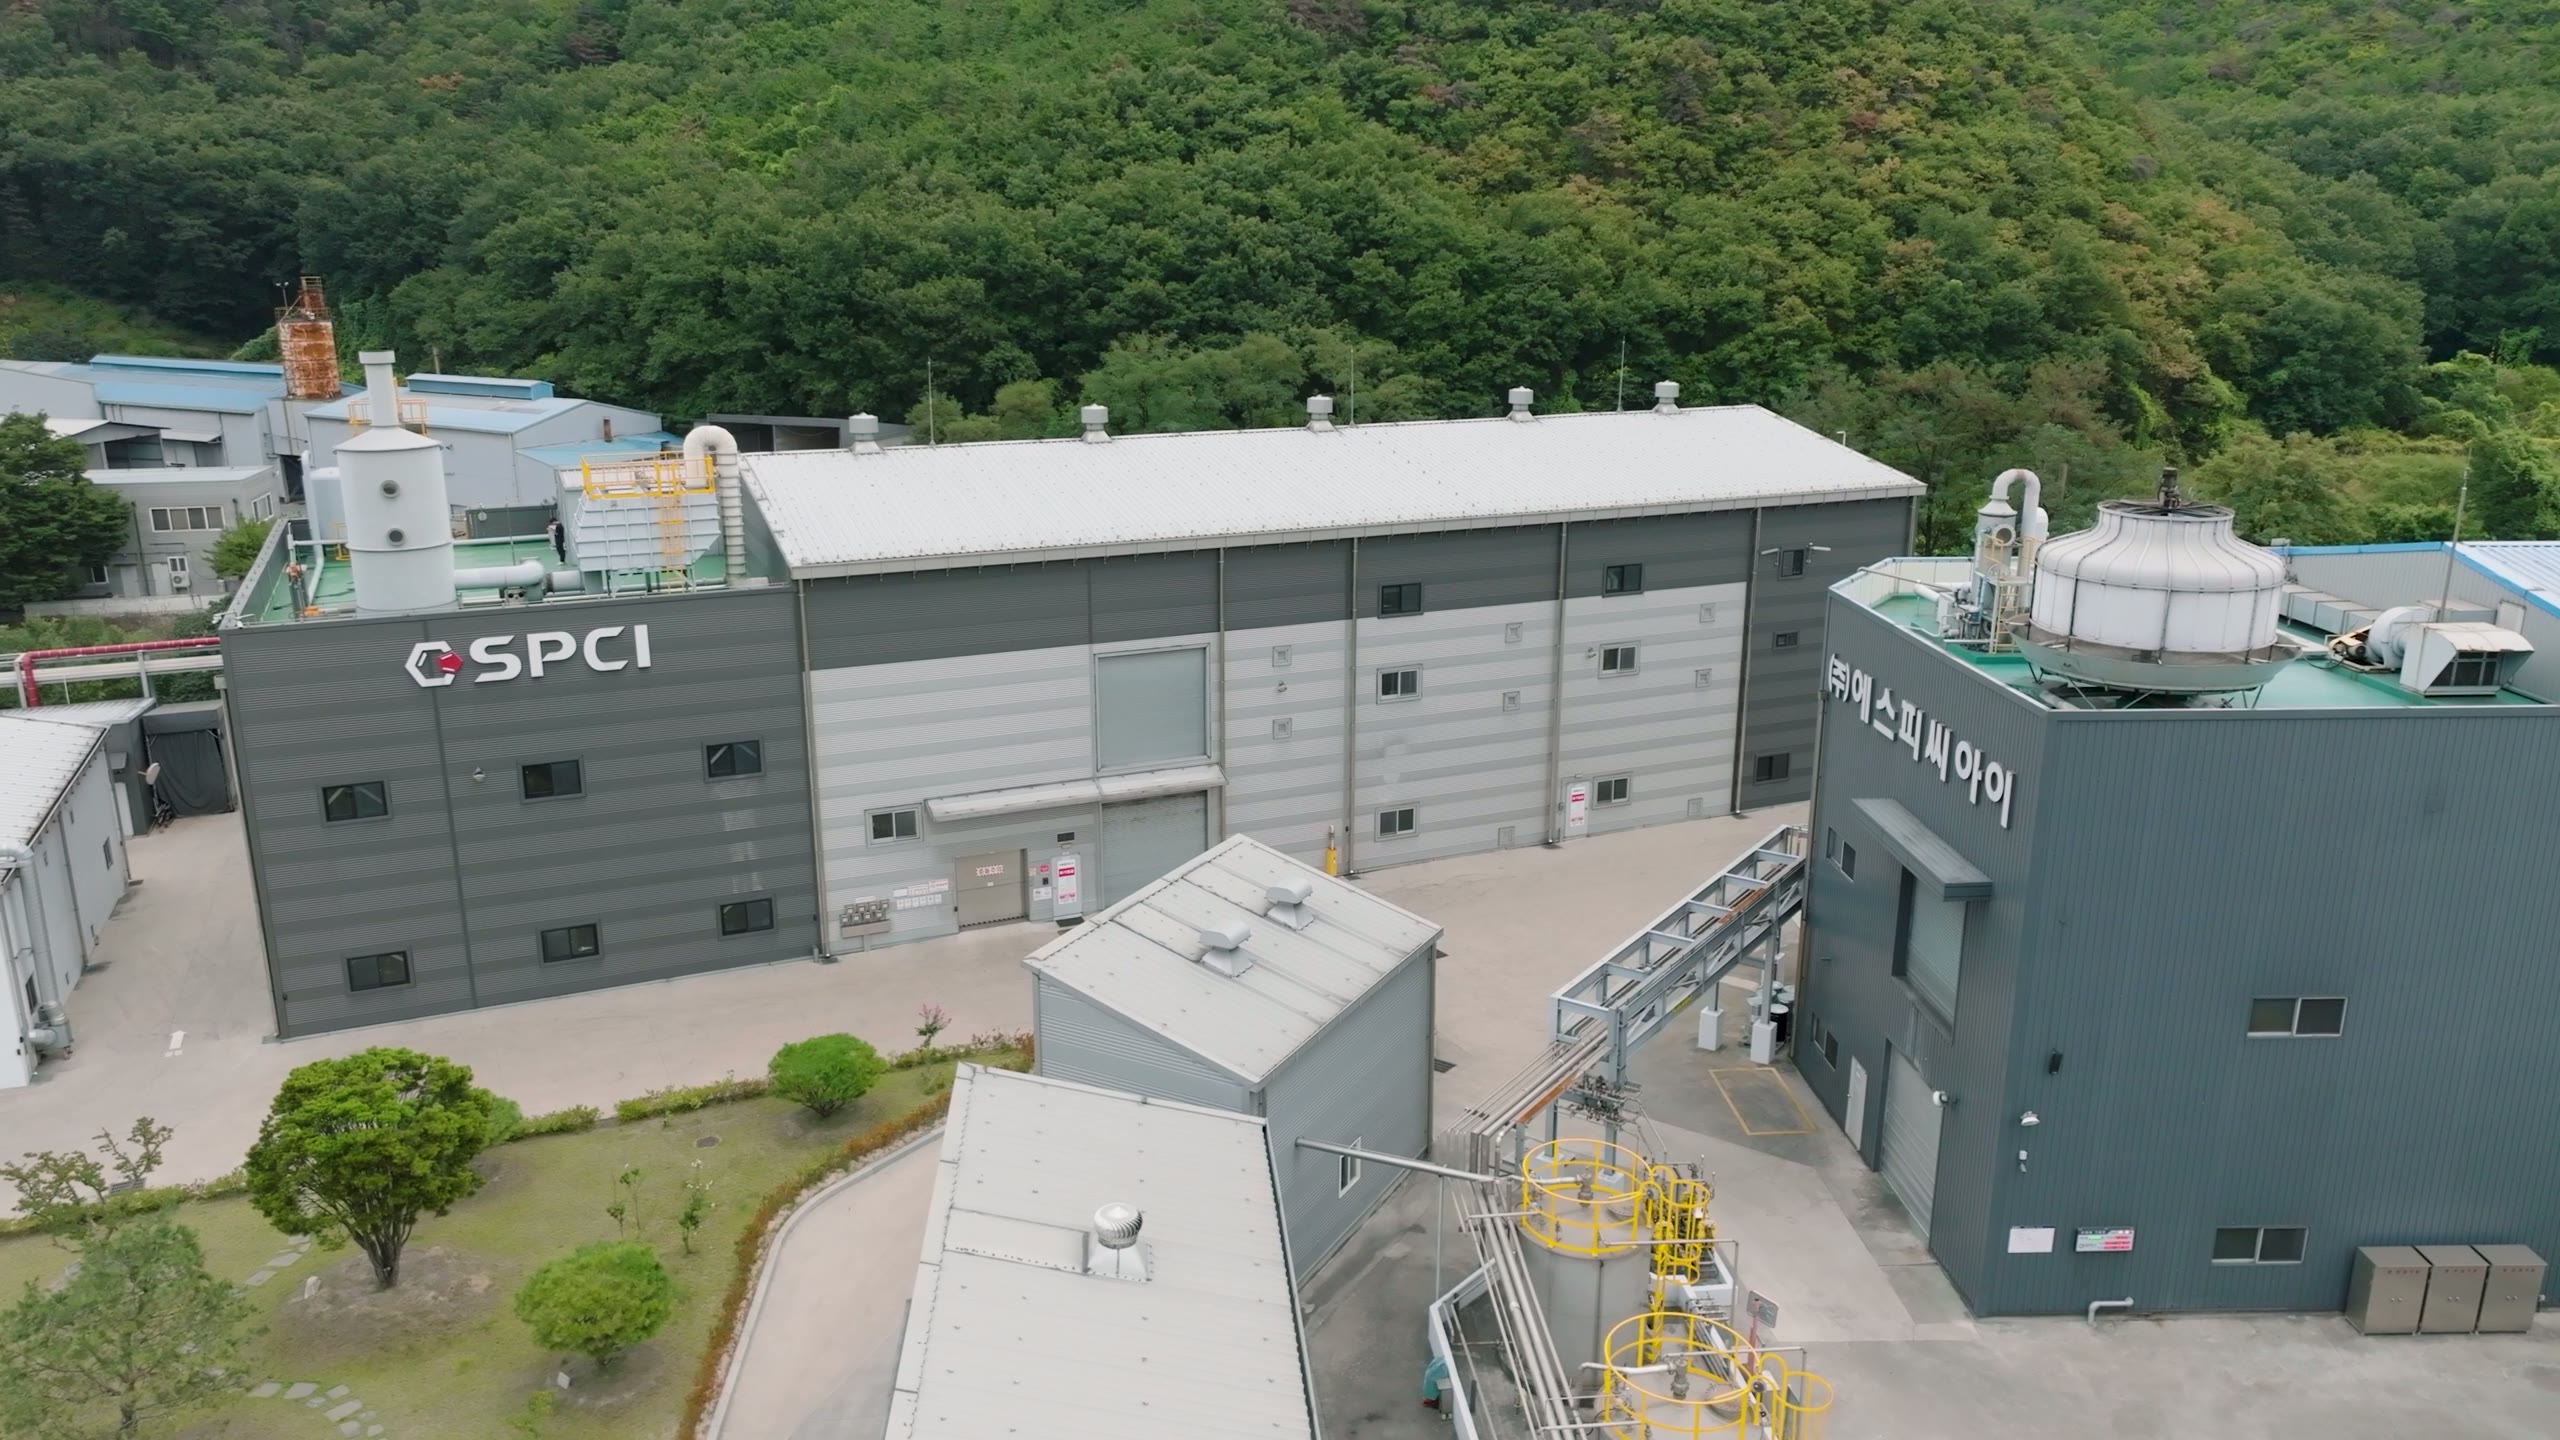
SPCI, Your ODM Partner

From new material development to commercialization,
SPCI partners with customers throughout the entire process—from initial development to commercial-scale production.

01/ 03

SCROLL

Technology, Facilities and Products

Moisture- and Oxygen-Controlled Processing Technology

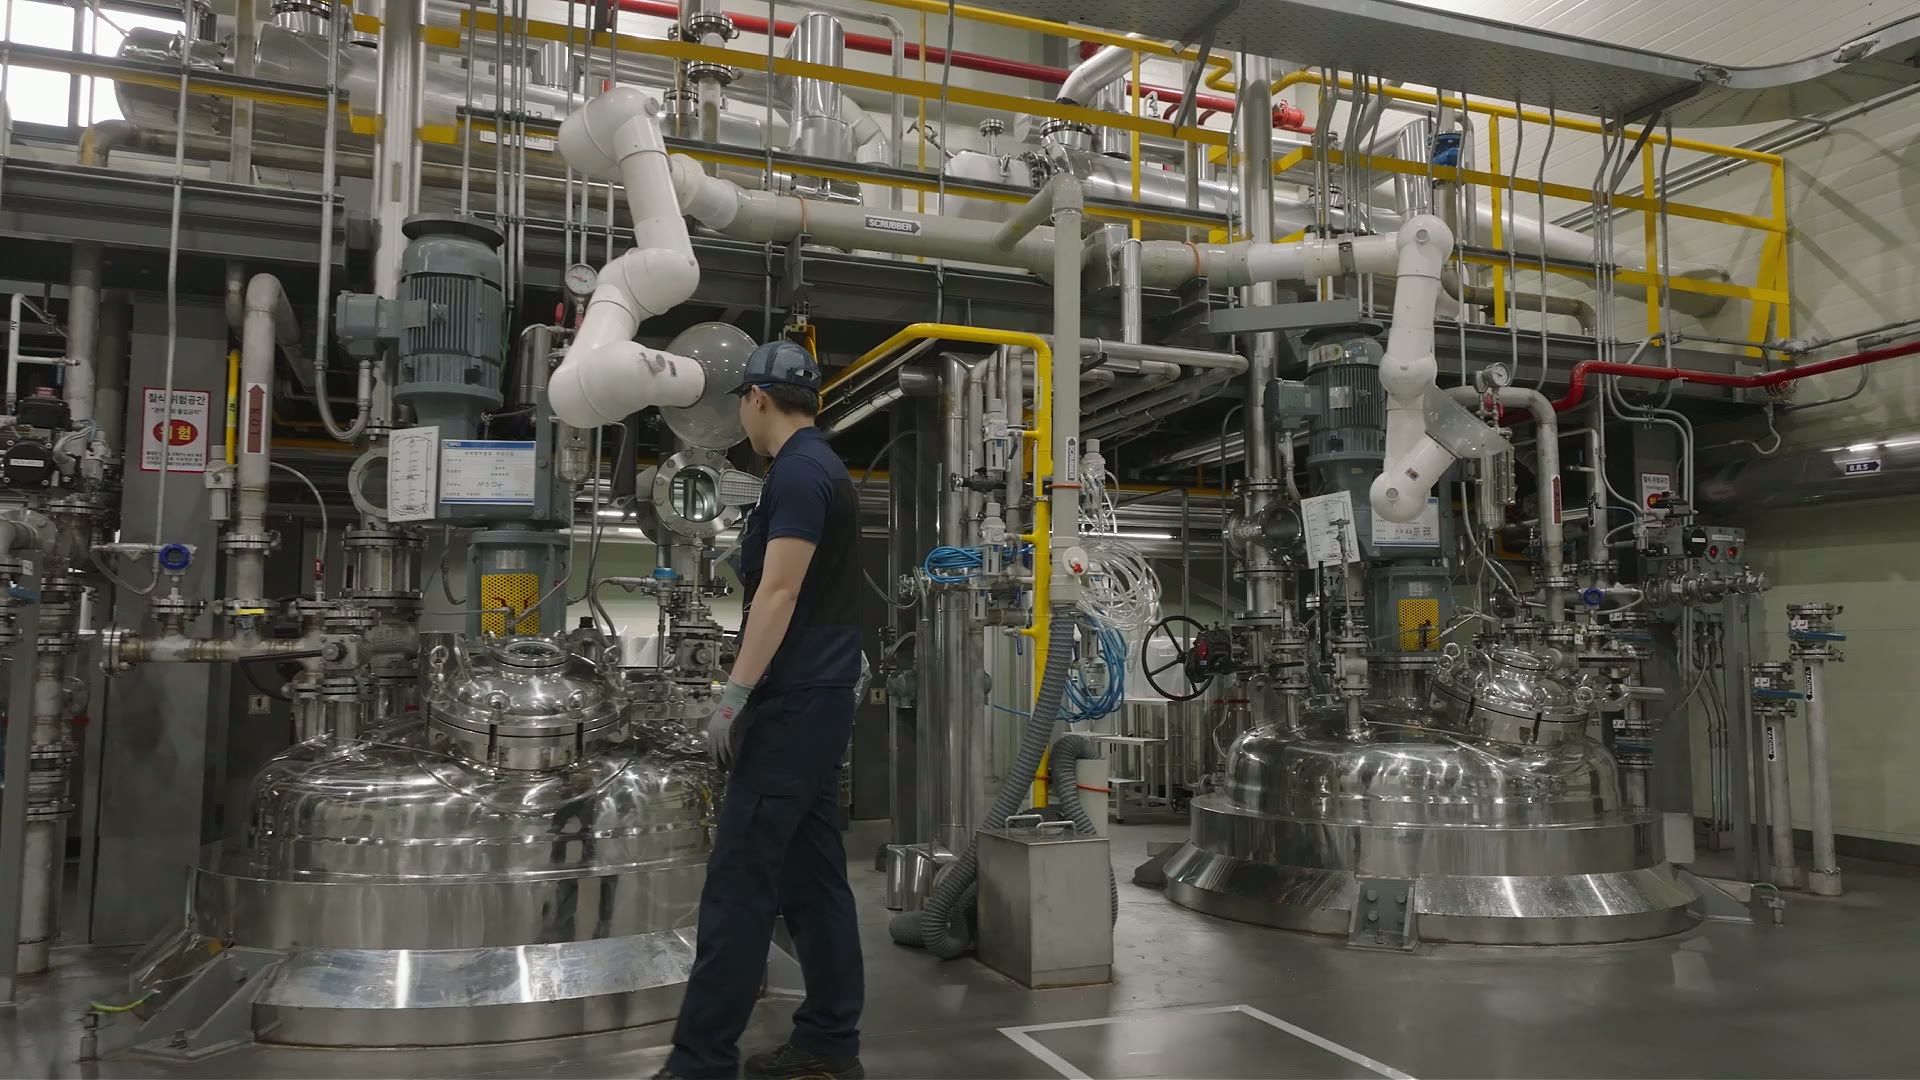
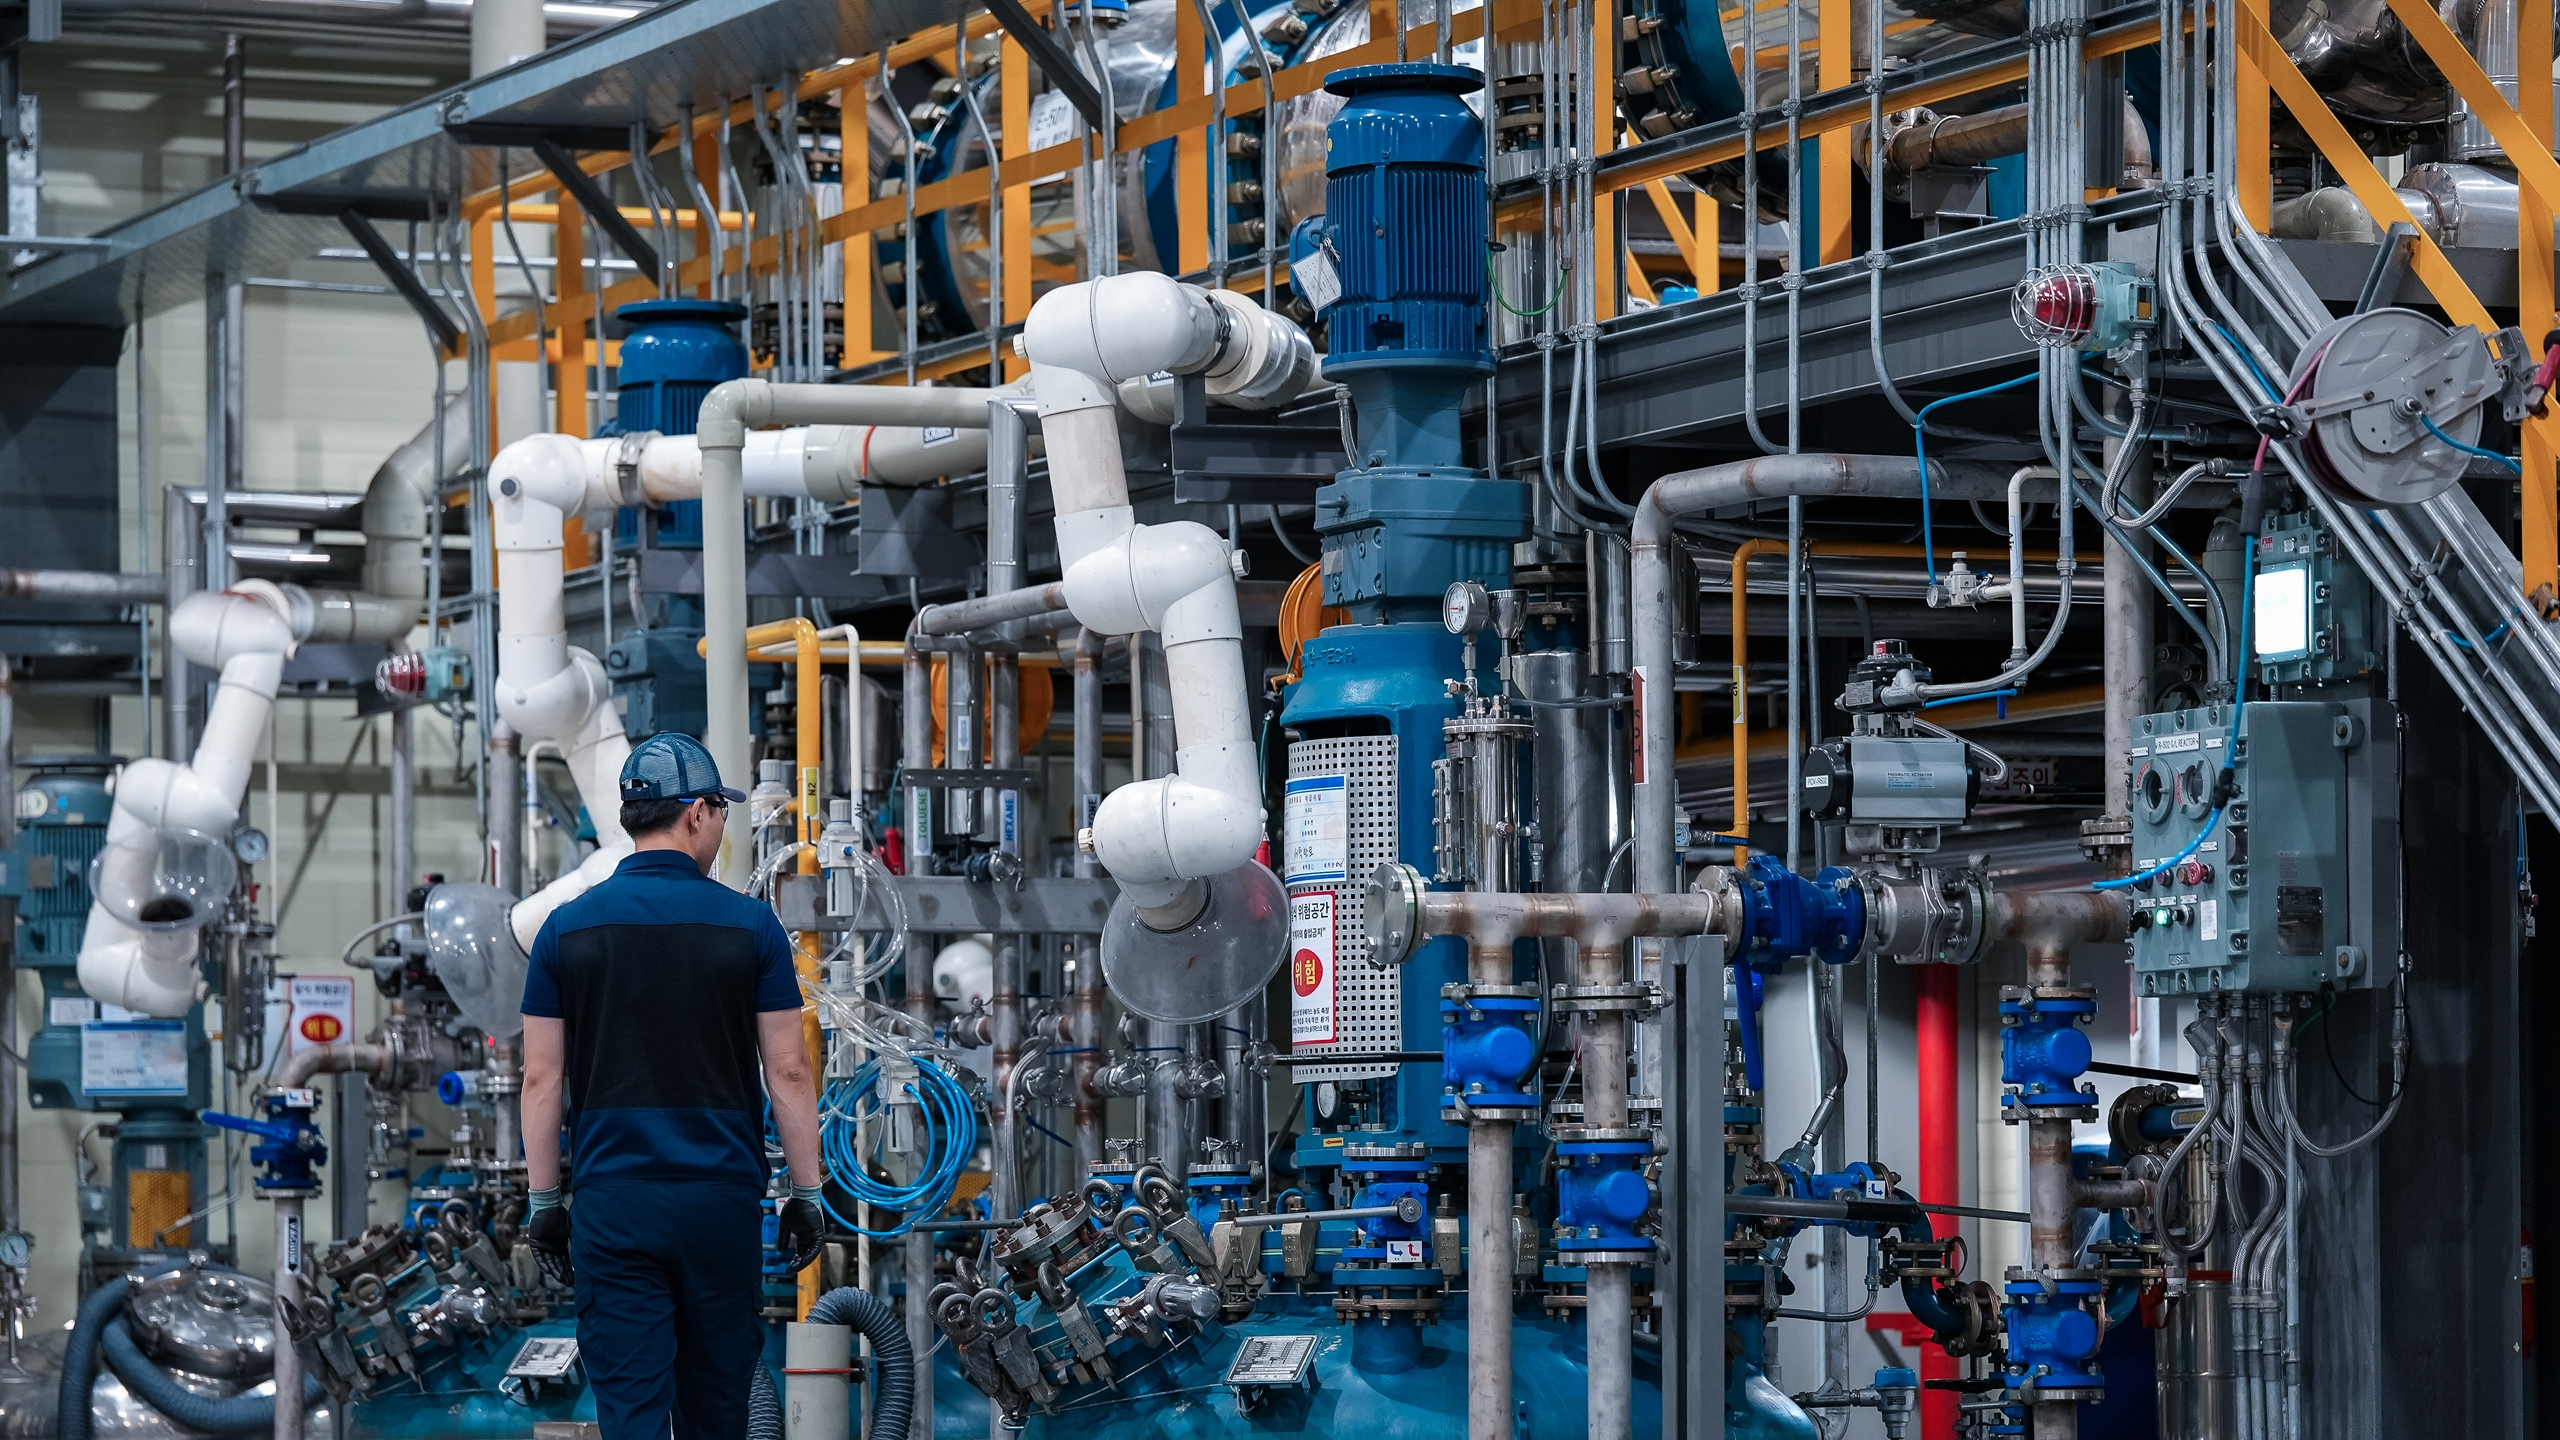
Our integrated production technology maintains controlled conditions throughout the process, from raw material charging to packaging, minimizing product exposure to oxygen and moisture.

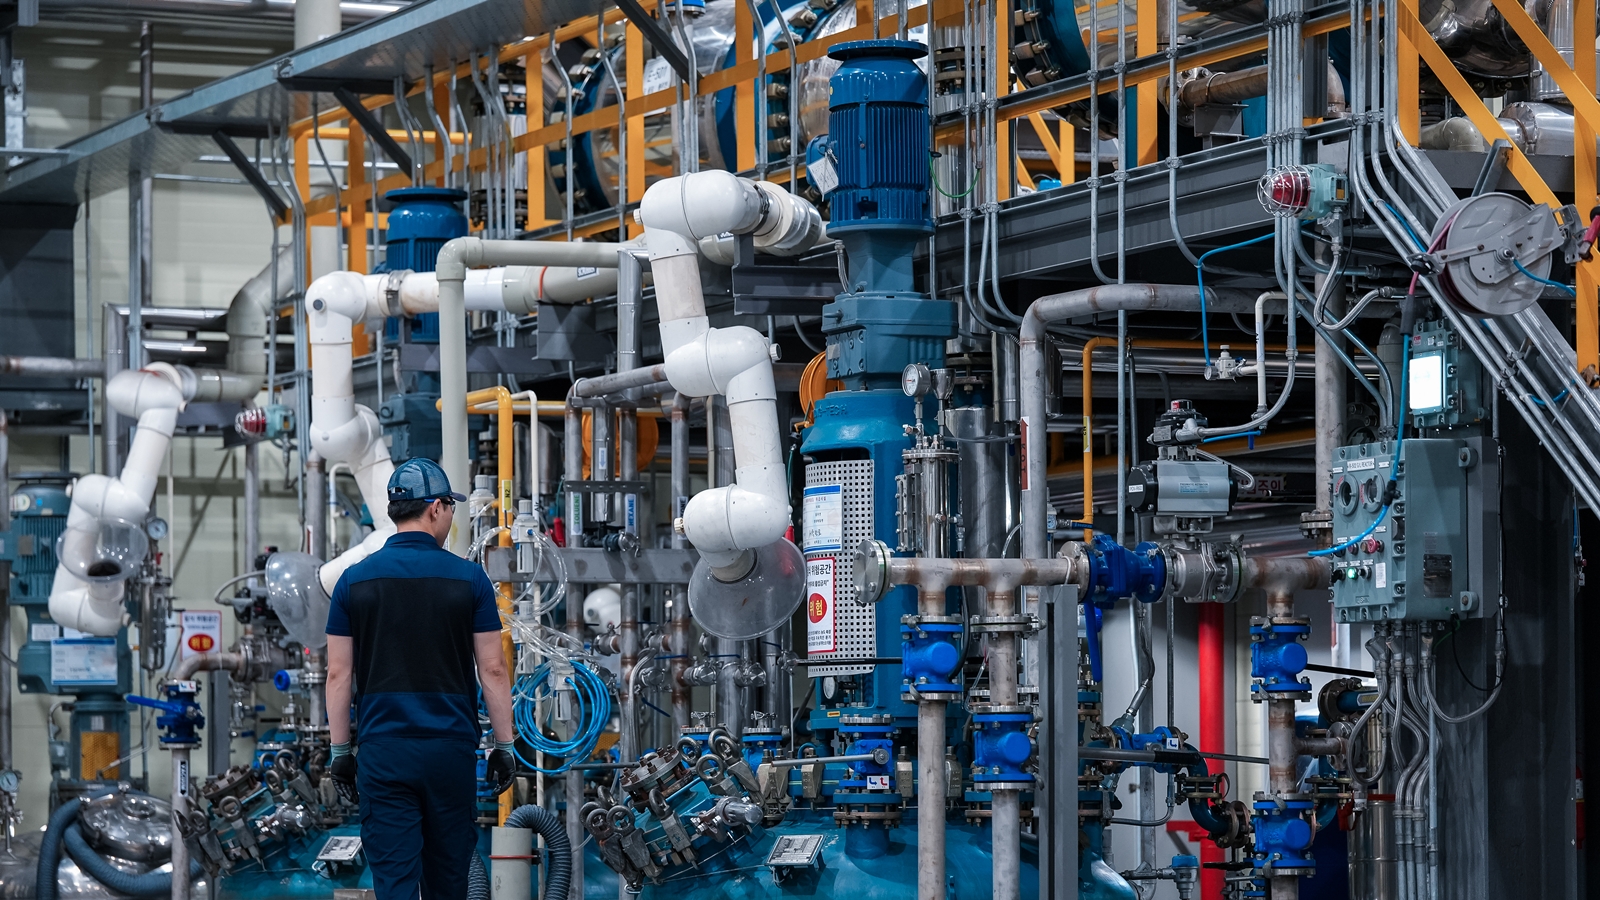
SPCI production process carried out in a sealed, inert atmosphere
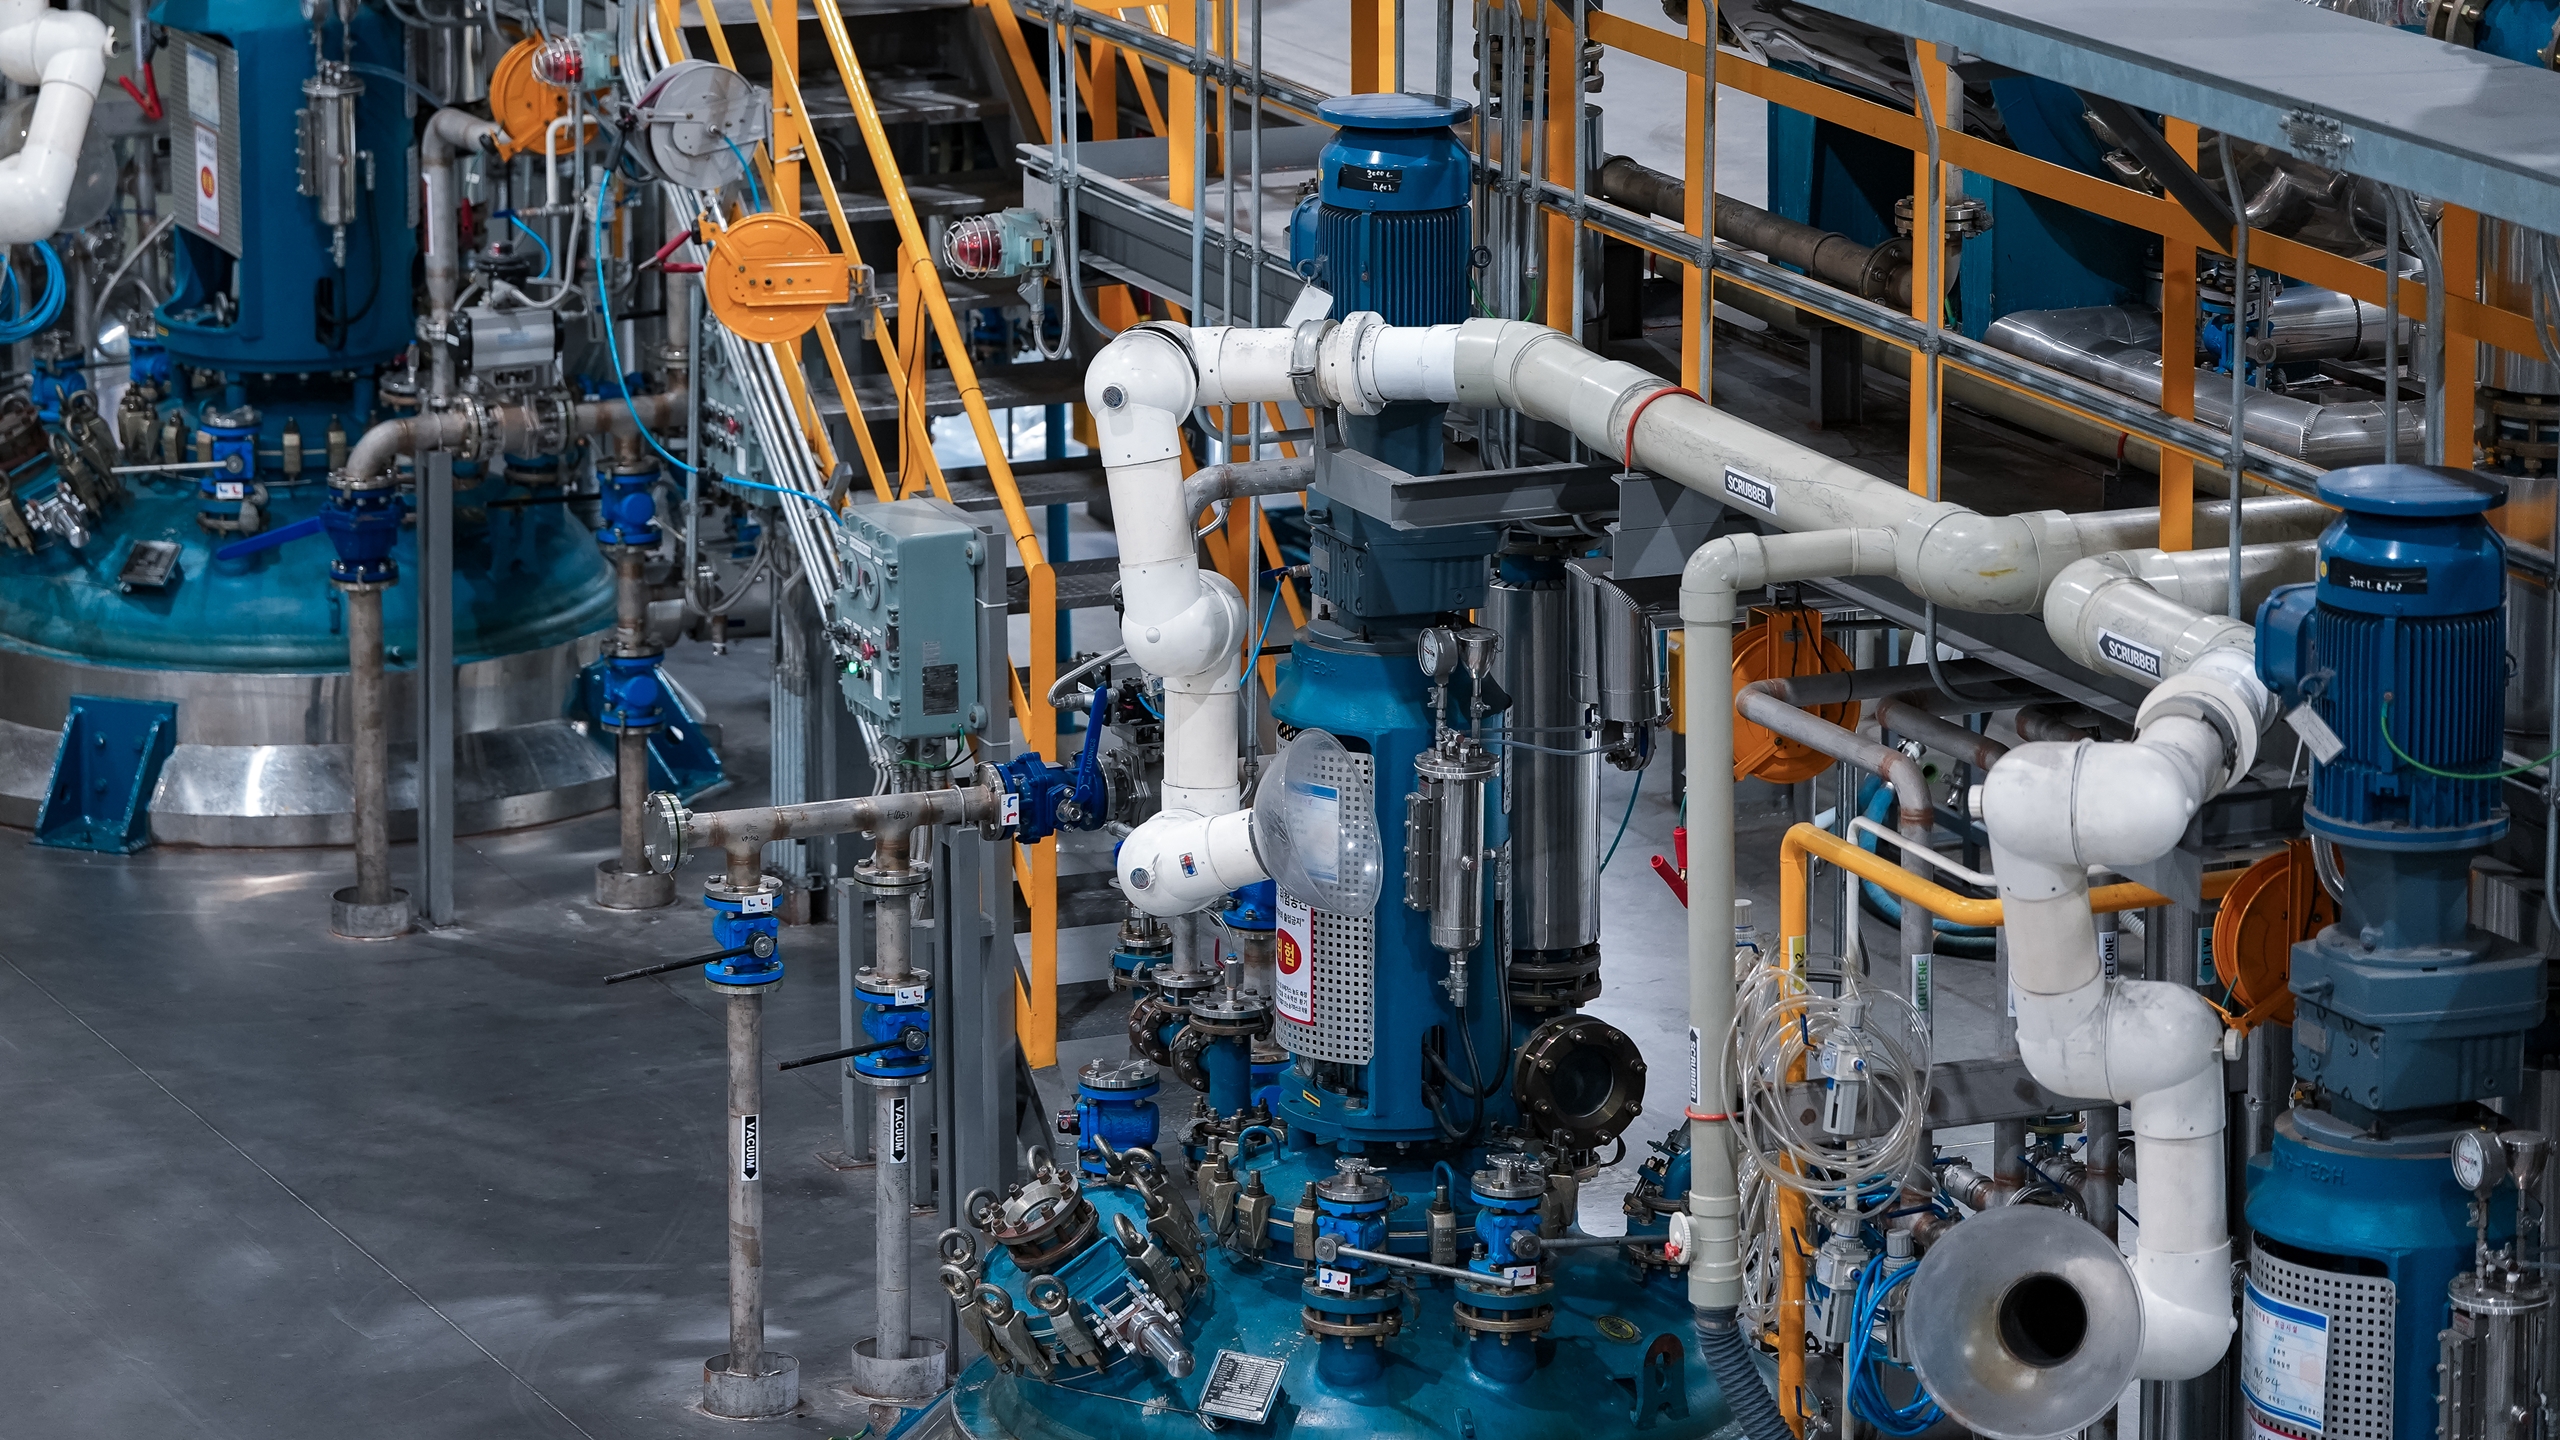
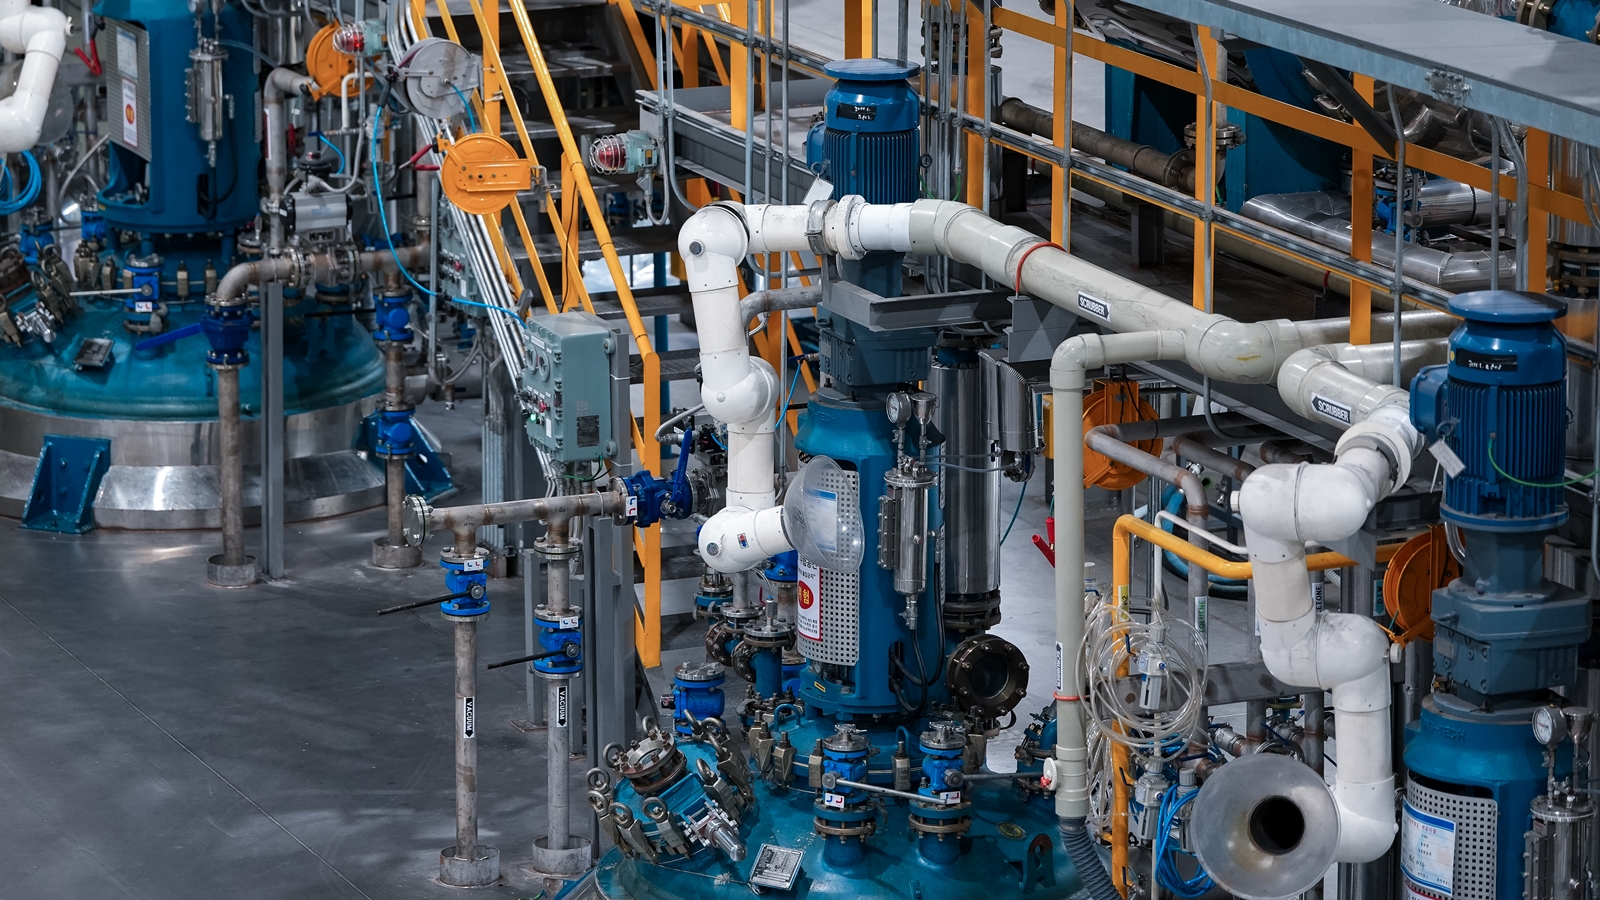
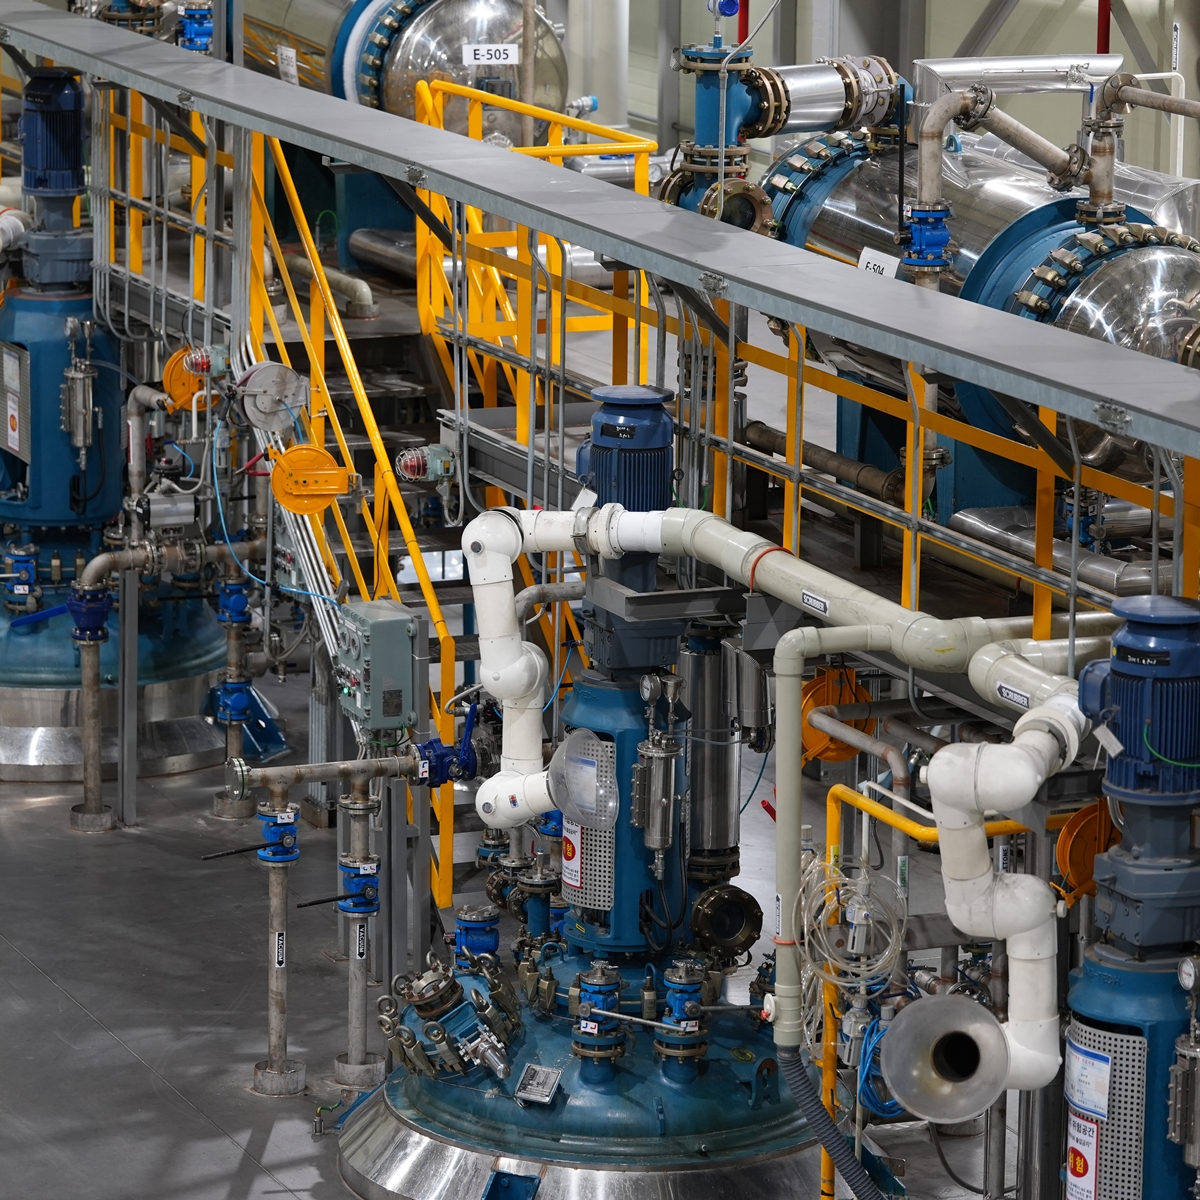
SPCI production floor lined with reaction and purification equipment
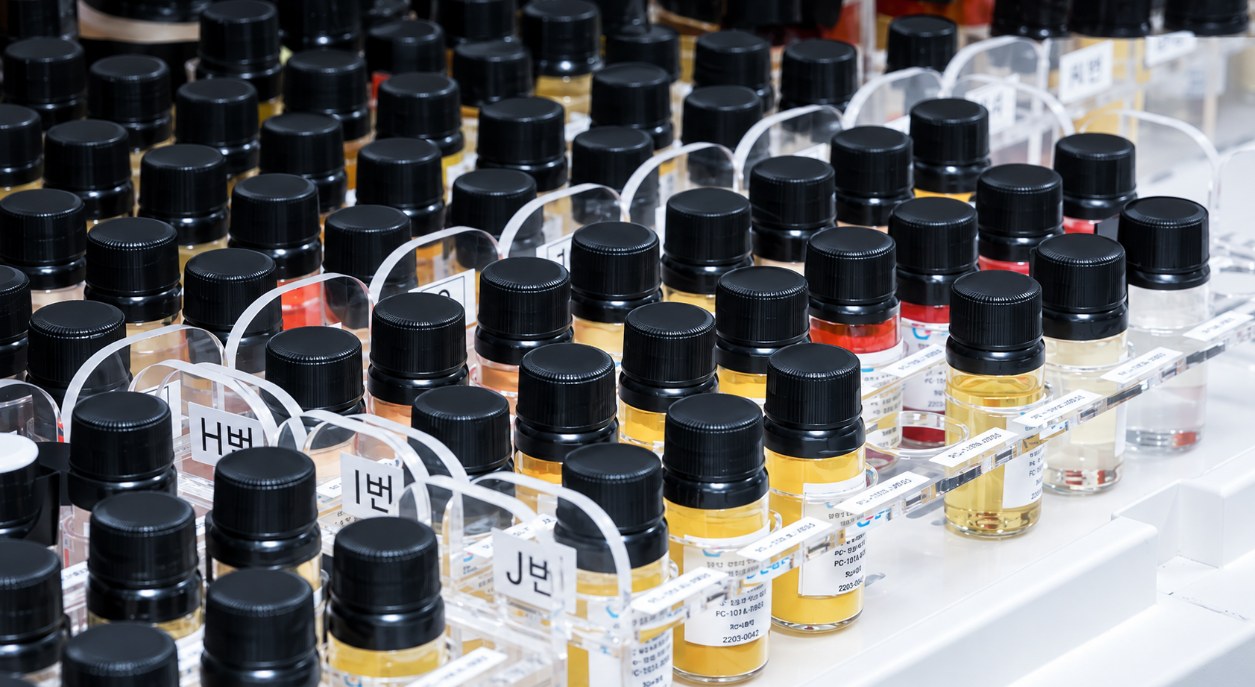
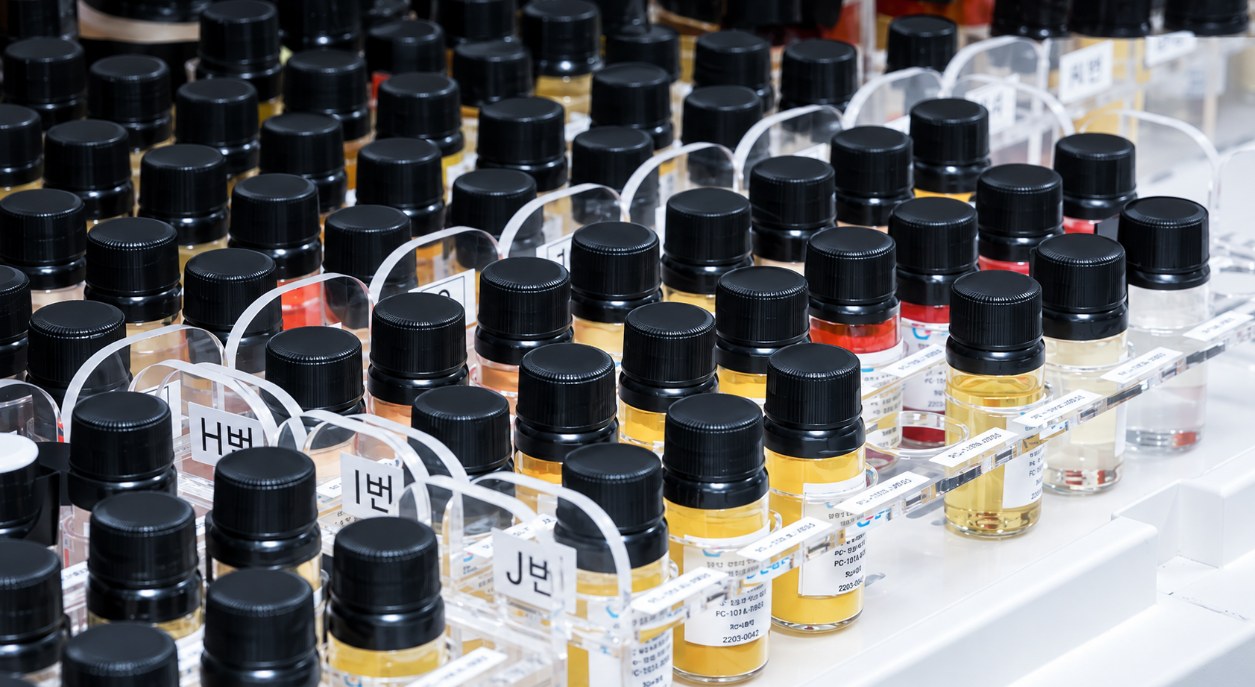
SPCI product materials

FACILITIES

Infrastructure Enabling
Commercial-Scale Production

Every stage of production—from reaction and purification to safety management
and quality verification—is carried out using our in-house facilities and equipment.

  1. Scale-up reactors of various capacities

    Scale-up Reactors

    Reactors of Various Capacities

    Our reactors range from small to large capacities,
    enabling us to accommodate different production
    volumes with flexibility and reliability.

    Total 26Plant 1: 6Plant 2: 10Plant 3: 10Maximum capacity: 10,000 L

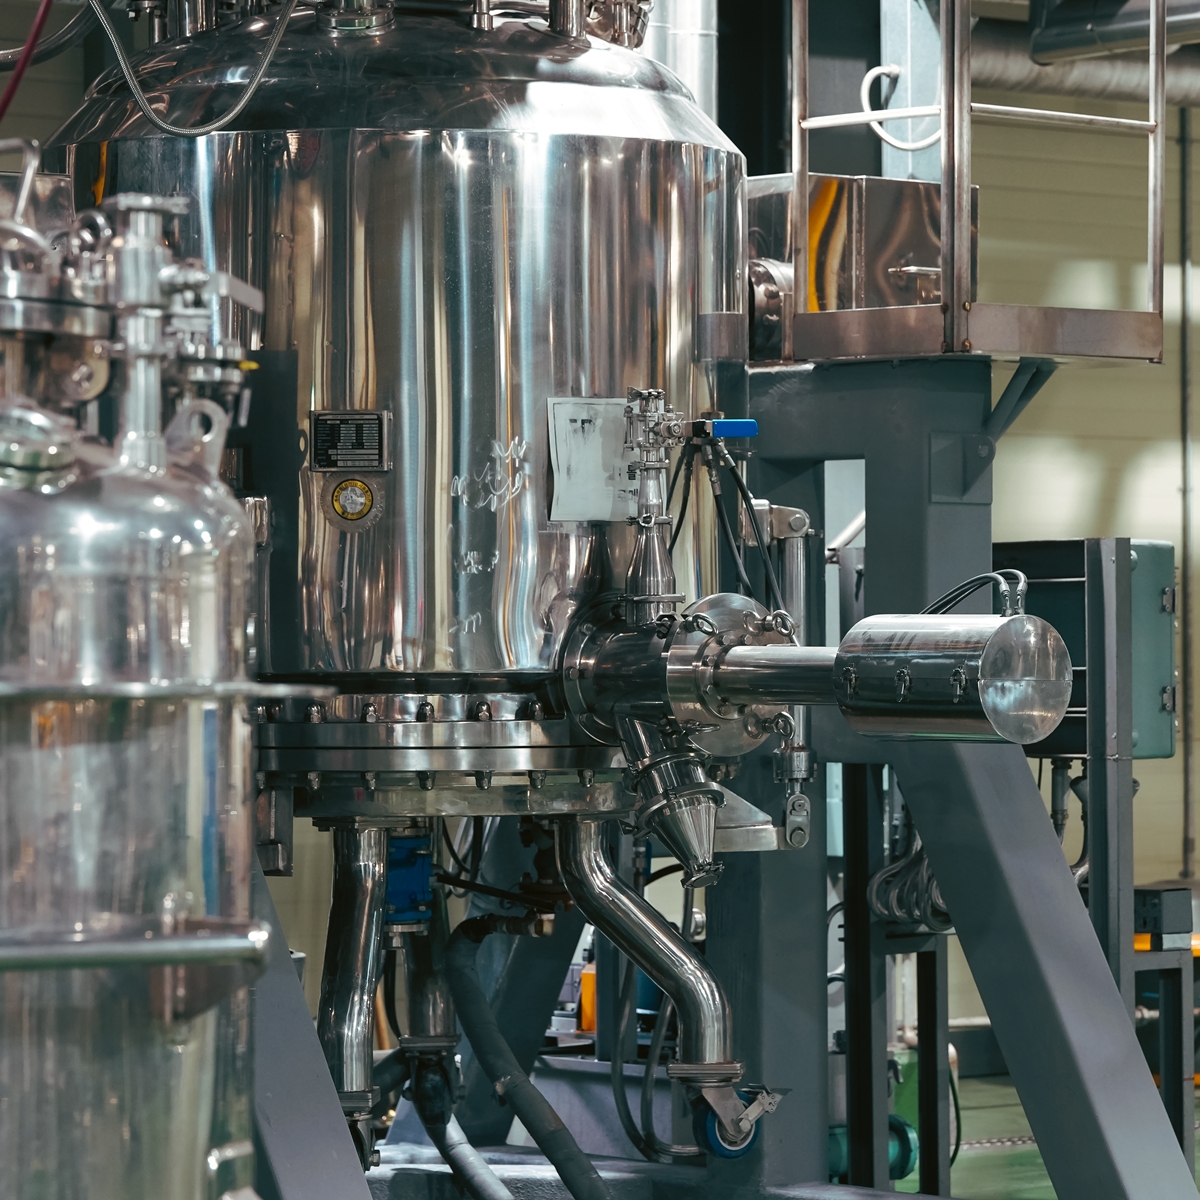
  2. Purification and drying equipment

    Purification & Drying

    Purification and Drying

    Our purification and drying processes remove
    impurities and moisture, helping us achieve
    the high purity required by our customers.

    Filter DryersPurificationDrying

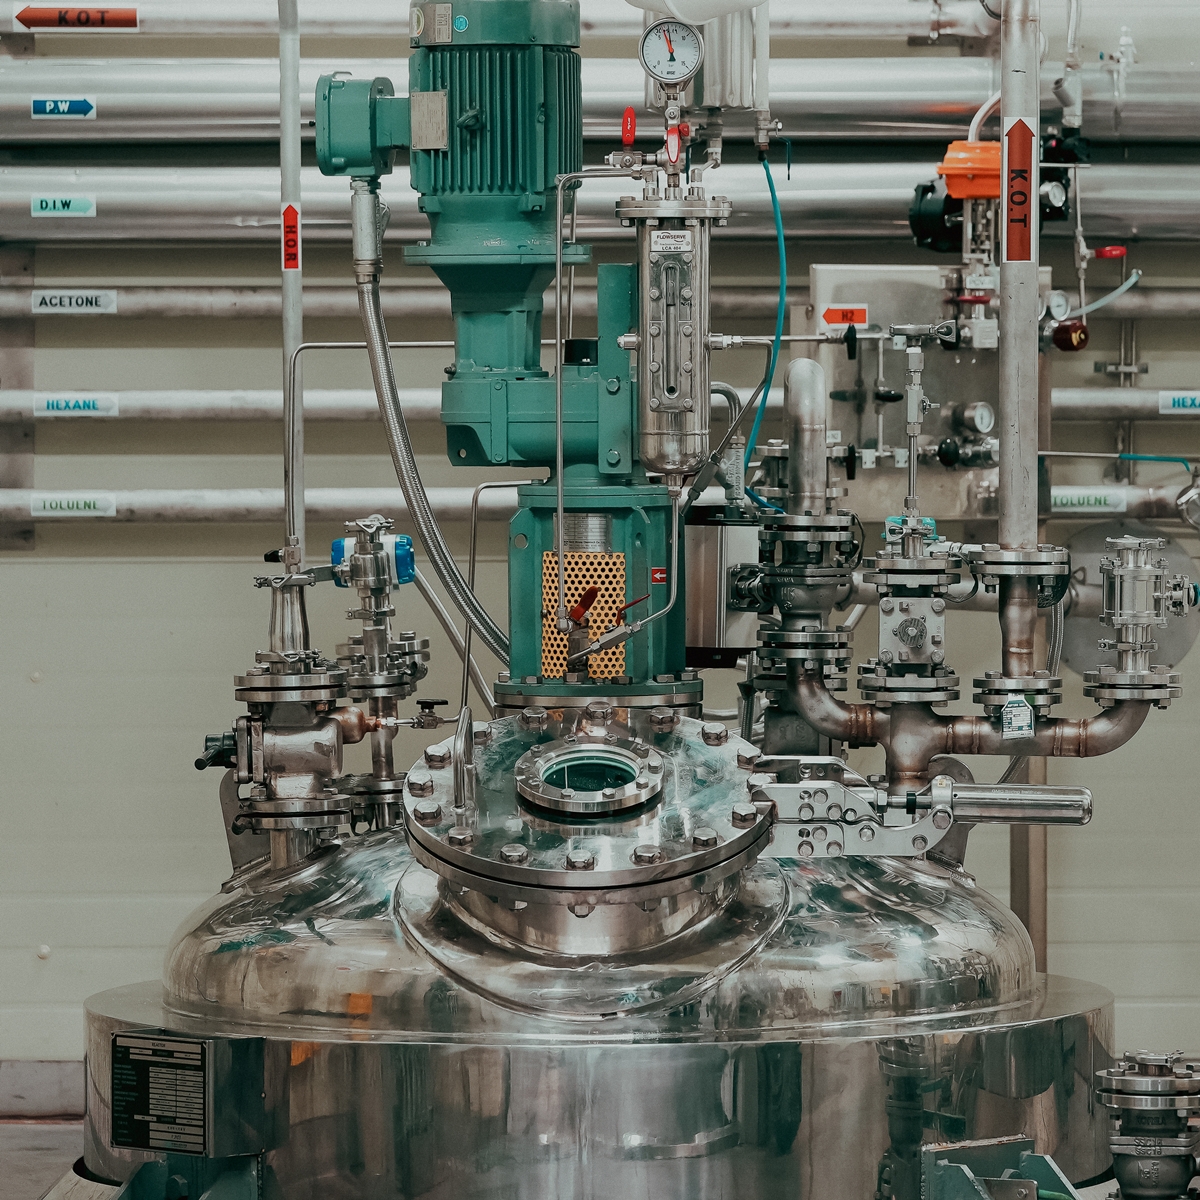
  3. High-pressure reactor for high-temperature, high-pressure reactions

    High-Pressure Reactors

    High-Pressure Reactors

    Our high-pressure reactors accommodate specialized
    reactions requiring elevated temperatures and pressures,
    enabling us to perform challenging processes in-house.

    High-Temperature/High-Pressure ReactionsSpecial Processes

  4. Specialized equipment including ozone and ultrapure water systems

    Specialized Facilities

    Specialized Equipment

    We operate specialized equipment and systems essential for
    high-purity material production, including ozone systems, ejectors,
    ultrapure water systems, and dedicated storage facilities for raw materials and finished products.

    Ozone SystemsEjectorsUltrapure Water SystemsRaw Material and Product Storage Facilities

Materials
by Industry

We supply high-purity materials for advanced industries, including the semiconductor and plastics sectors, with products tailored to each customer’s processes.

Business areas

Expanding Business Areas

Metallocenes

Key Raw Materials for High-Performance Polyolefins

  • Development and large-scale production of metallocene precursors
  • One-stop system from metallocene precursors to supported catalysts
  • Securing global market share through expanded exports

Electronic Materials

A Future Growth Driver with High Profitability

  • Next-generation semiconductor materials, including high-k and low-k precursors and intermediates
  • Advanced high-purity purification technology

Specialty Chemicals

MLCC Binder Materials

  • Development and commercial production of advanced MLCC materials
  • Development of sodium metal forming technology and supply of core materials
  • Development and commercial production of materials for biotechnology and pharmaceutical applications
  • Patented chromium catalyst technologies and commercial catalyst supply

Bulk Materials

Commercial Production and ODM/OEM Capabilities

  • Supply of NdBR catalysts and commercial-scale HNBR production
  • Support system for large-volume ODM/OEM supply

Building on its metallocene catalyst manufacturing expertise,

with capabilities spanning supported catalysts, advanced MLCC materials, and bulk materials, SPCI is evolving into

a Technology Platform Company

Step-by-Step Scale-Up
From Laboratory to Plant

SPCI works closely with customers at every stage of process scale-up,
from evaluating the feasibility of a new material
to establishing stable commercial-production conditions.

By the numbers

SPCI
by the Numbers

150+Materials

Developed to Date

CUMULATIVE

2009

Establishment of SPCI

SINCE 2009

Our extensive research and manufacturing experience serves as the foundation for accelerating the commercialization of customers’ materials.

26

Reactors Owned

REACTORS

10,000L

Maximum Batch Capacity

MAX BATCH

As of September 2026
Figures include the expansion of Plant 3.

40+Companies

Customers Served

PARTNERS

12Patents

Granted and Pending

PATENTS

Technology and Trust
The Foundation of Our Customer Partnerships

Catalyst and fine chemical production site

01

Manufacturing Experience

Drawing on expertise accumulated since 2009 in catalyst and fine chemical production, SPCI consistently manufactures advanced materials that meet customer requirements.

02

Quality Assurance

From the receipt of raw materials to final shipment, we maintain the required levels of purity and quality through verification at every stage of production.

03

Collaborative Development

We build ODM partnerships by working alongside customers from early-stage research and material development through commercial-scale production.